Aug 21, 2026
In PET extrusion, maintaining a stable melt temperature is essential for product quality and uninterrupted production. The backflush filter removes contaminants from molten PET without stopping the extrusion line, but this process only works when the filter housing stays at a consistently high temperature. If the temperature drops, PET quickly solidifies, leading to pressure increases, clogged screens, and costly downtime.
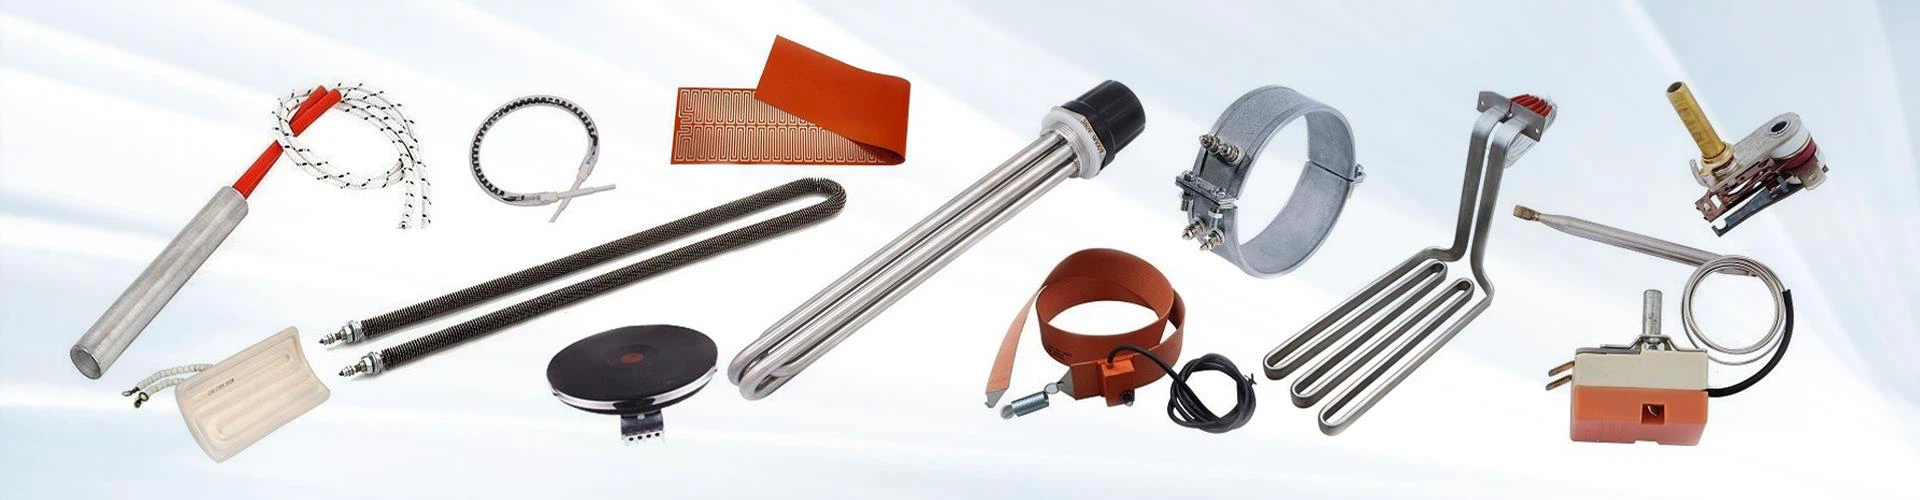
This is why cartridge heaters are widely used in PET extruder backflush filters. Their compact design, high watt density, and excellent heat transfer make them ideal for heating filter blocks and manifolds in demanding extrusion environments.
A backflush filter is installed between the extruder and the die head to continuously remove impurities from molten PET. Unlike manual screen changers, it automatically cleans or replaces contaminated filter screens while production continues.
The filter housing typically operates at temperatures between 260°C and 320°C, depending on the PET formulation and processing conditions. Heating must remain uniform throughout the filter body to prevent cold spots where polymer could crystallize or solidify.

Cartridge heaters can operate reliably at temperatures exceeding 700°C internally, providing ample thermal capacity for PET processing while maintaining stable surface temperatures in the filter block.
Backflush filters often have limited installation space but require significant heating power. Cartridge heaters deliver 10–30 W/cm² or higher, allowing rapid heat-up and efficient temperature recovery after each backflush cycle.
Precision-manufactured cartridge heaters provide even heat along their heated length, minimizing temperature gradients inside the filter housing and helping maintain consistent melt viscosity.
With stainless steel sheaths, high-purity magnesium oxide insulation, and nickel-chromium resistance wire, cartridge heaters withstand continuous high-temperature operation and frequent thermal cycling common in extrusion systems.
When selecting a cartridge heater for PET backflush filters, engineers should consider more than voltage and wattage.
| Parameter | Typical Recommendation |
|---|---|
| Sheath material | Stainless steel 304 / 316 or Incoloy |
| Operating temperature | 260–320°C for PET processing |
| Watt density | 10–30 W/cm² (depending on installation) |
| Fit tolerance | H7 precision bore for optimal heat transfer |
| Thermocouple | Type J or K integrated option |
| Lead protection | High-temperature fiberglass or ceramic leads |
A close mechanical fit between the heater and the drilled hole is especially important. Poor contact creates air gaps that reduce heat transfer and significantly shorten heater life.
Modern PET recycling lines process increasingly contaminated materials, making efficient filtration more critical than ever. Reliable cartridge heating helps manufacturers achieve:
The PET extruder backflush filter depends on precise, continuous heating to maintain molten polymer flow and ensure uninterrupted filtration.
Cartridge heaters provide the high-temperature capability, compact size, and high power density needed for this demanding application, making them one of the most effective heating solutions for PET extrusion equipment.
For custom backflush filter projects, cartridge heaters can be engineered with specific diameters, heated lengths, watt densities, thermocouple integration, and lead configurations to match virtually any PET extrusion system.

Send your inquiry about cosmetic tubes to us and experience the transformative power it can have on your business.
Previous: How Are NTC Sensors Used in Free Cooling Devices for Cold-Climate Data Centers?
Next: How Do U-Shaped Resistors Improve Elevator Braking Performance?